Slip casting is a forming technique in which a deflocculated clay slip is poured into an absorbent plaster mold; the plaster draws water out of the slip against the mold wall, building up a solid layer of clay, after which the excess slip is poured back out and the cast piece is removed once it has stiffened enough to hold its own shape. Unlike wheel throwing or handbuilding, it shapes clay in its liquid state rather than its plastic state, and needs a mold rather than direct hand contact with the final form.
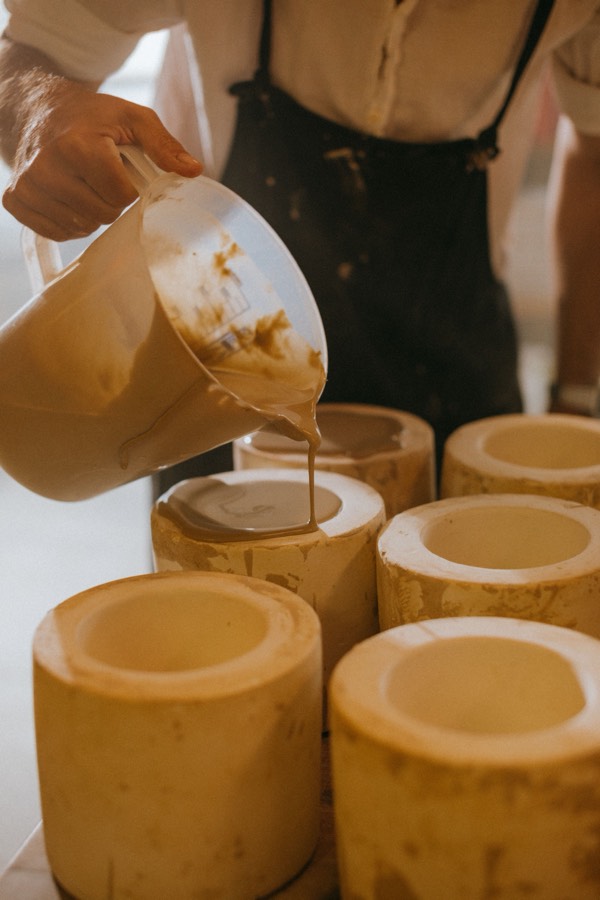
¶ How it works
A casting slip, a specially formulated clay body deflocculated into a fluid, pourable liquid with very little water relative to an ordinary throwing or handbuilding consistency (see casting bodies), is poured to fill a plaster mold completely. The plaster is porous and absorbs water out of the slip nearest the mold wall, building up a layer of stiffening clay against that wall over a period of minutes; once the layer reaches the desired thickness, the still-liquid slip in the center is poured back out, leaving a hollow-cast shell (drain casting), or the mold is left full to cast a solid piece (solid casting) where the whole form is meant to be filled rather than hollow. After a further period firming up in the mold, the mold is opened and the cast piece removed, still soft enough to trim seams but firm enough to hold its shape unsupported.
¶ Practical considerations
A single plaster mold, generally built in two or more pieces so it can be opened and closed around the cast, can produce many identical pieces before it wears out, which makes slip casting the standard choice for reproducible production runs and for complex or undercut shapes that neither a wheel nor handbuilding could form directly, such as a piece with a narrow neck and a wide body, or fine surface detail transferred straight from the mold. The tradeoff is the upfront cost of making the mold itself, usually cast from an original model, and the fact that plaster molds absorb water more slowly as they age and eventually need replacing. A multi-piece mold's sections are held together with straps or heavy rubber bands while filled, and leave a thin mold line or seam where the sections met, which is trimmed and smoothed away from the cast piece once it is firm enough to handle but still soft enough to cut cleanly.
¶ References
- Hansen, Tony. "Slip Casting." Digitalfire Reference Library. digitalfire.com
- Photo by KoolShooters, via Pexels, Pexels License (resized and re-compressed from the original).